A few micrometers can do wonders✨
Nowadays, we want to produce products as quickly as possible and thus make the most of our machines, which brings us greater profit. How do we achieve such productivity?
We can improve or refine the tool path, but when that is no longer enough, we want to increase the speeds and feeds of the tool. This is where a small problem can arise. Tools are usually made of carbide, which can withstand loads only up to a certain point, and anything beyond that can ultimately result in tool breakage. As a result of the continuous development of production processes, protective PVD coatings were developed, and they have been established in industry for many years. It all started with the gold TiN coating, which is still used in some places, but in most applications it has been replaced by special coatings intended only for certain materials.
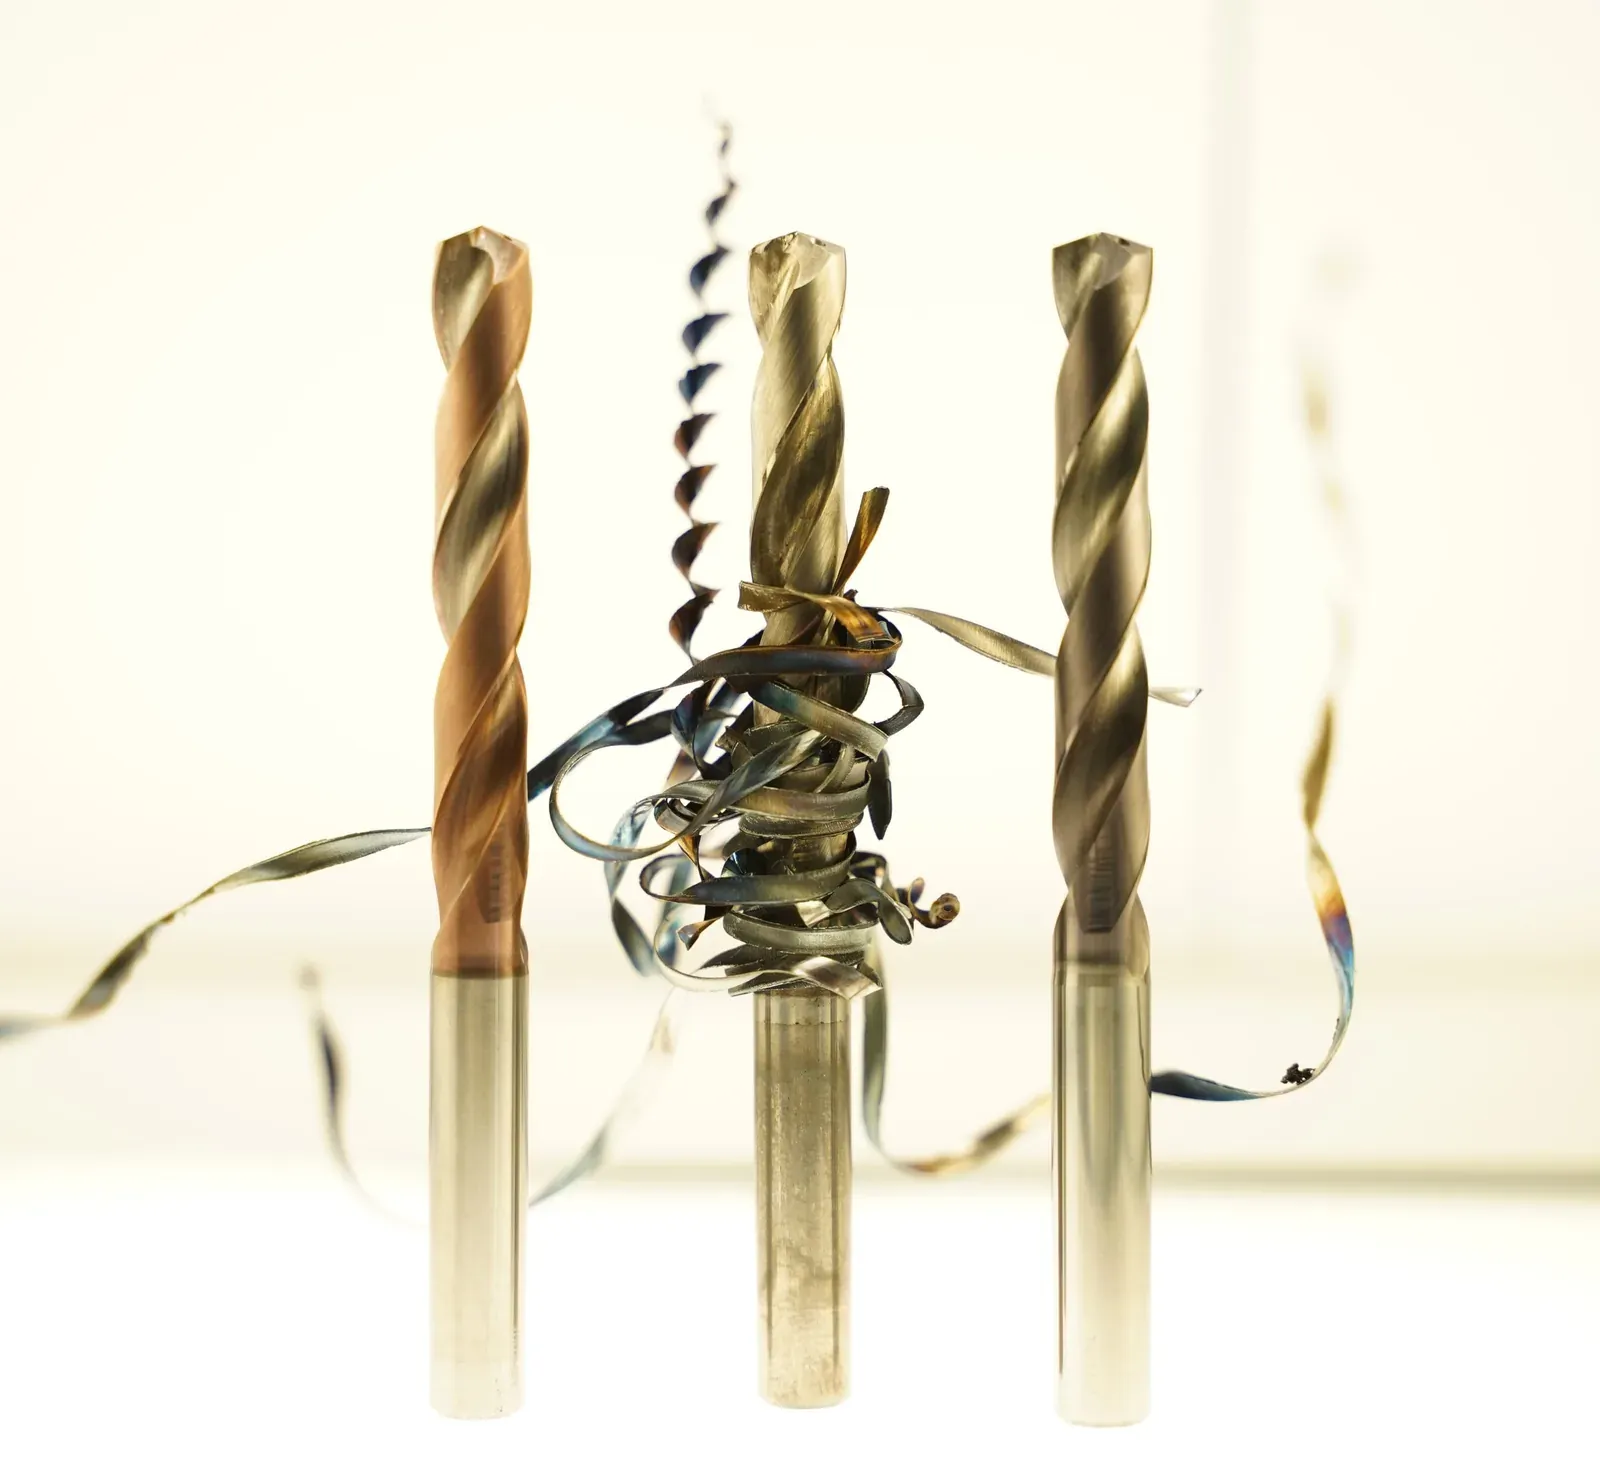
We wanted to see for ourselves what impact the correct choice of coating has on the life of the cutting tool itself, so we tested milling cutters and drills refined with different coatings when machining carbon steel OCR (1.2379) and hardened steel 42CrMo4. This article presents one part of the testing - drilling with a Ø8 drill in 42CrMo4 steel. We compared an uncoated drill with a Ti4Al-coated drill and a 4HARD-coated drill, all of which had a similar initial runout of 12 µm on the diameter and were exposed to the same machining conditions.
Ti4Al as well as 4HARD are the latest generation of PVD coatings, which have a very fine-grained structure and a very smooth surface and do not round the cutting edge. The 4HARD coating is intended for machining very hard hardened materials; at the same time it is highly resistant to high temperatures and extremely suitable for machining without cooling. The Ti4Al coating is used for machining all types of steel up to a hardness of around 55 HRC, which makes this coating the first choice for the tested hardened steel 42CrMo4 with a hardness of 53 HRC.
Machining parameters:
- vc = 160 m/min
- f = 0.2 mm/rev
- L = 4xD
- emulsion cooling through the coolant channels
The upper wear limit was VB = 0.12 mm, which represents the wear on the cutting face. Of course, the VB criterion for resharpening or replacing the tool can be higher if we do not need to achieve a very smooth workpiece surface.
The coated drills reached the required criterion with different numbers of holes, while the uncoated drill had to stop machining prematurely, and the wear of its cutting edge significantly exceeded the set limit.
Test results:
- Uncoated drill: 18 holes
- Drill with 4HARD coating: 456 holes
- Drill with Ti4Al coating: 960 holes
The results and the picture show that an uncoated tool is not suitable for machining at high cutting parameters, but at the same time we see that the correct choice of PVD coating is also important, as the 4HARD coating is primarily intended for machining very hard materials, but with certain not-so-hard materials it achieves 50 % or even lower efficiency compared with the best currently available coatings.
That’s why we, a team of engineers and technologists, are here to advise you and select the best coating for your application!
Gazela d.o.o. Žan Dobrovnik Krško, 1 July 2021